Feeder & Shear Mechanism
Shear Shanks for IS-Machine Feeders
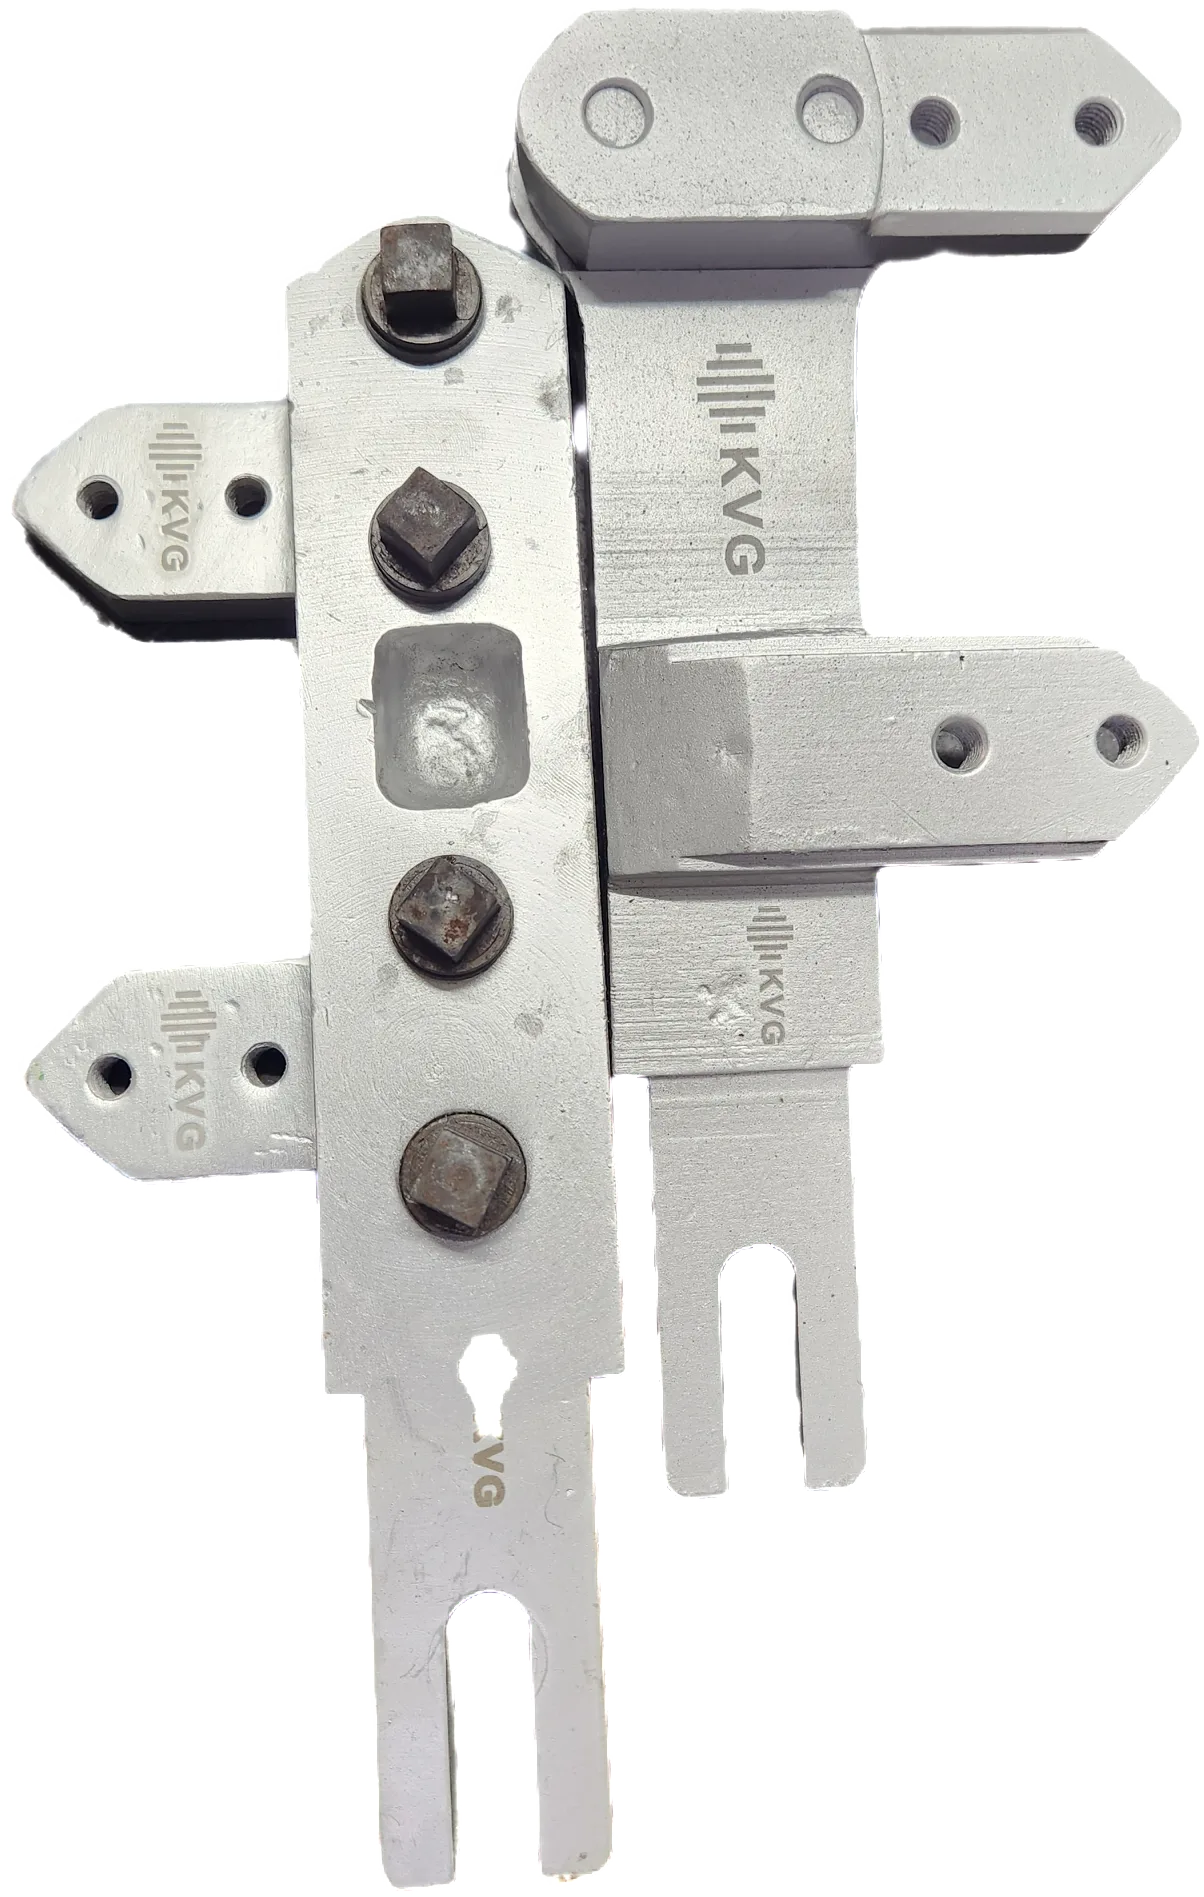
The shear shank carries the shear blades at the feeder, taking them through every cut so each gob is severed cleanly below the orifice at a repeatable weight.
Every gob on the machine starts with a cut. The shanks hold the blades, close them on the glass stream and open again, cycle after cycle. If the blades meet squarely and at the same point every time, the cut is clean, the weight repeats, and nothing is carried forward into the parison. If they do not, you get shear marks, tails and drifting weights.
So a shank is a holding job first. Blade seats machined flat, clamp faces true, mounting holes on the centres your drawing calls for — that is what holds a blade setting where you set it. It also works hot, in shear spray and glass dust, reversing on every cycle. Cast iron, SG iron and aluminium each trade stiffness against reciprocating mass, so we machine in the family your mechanism was built around.
What you get
Built for Repeatable Production
Machined to Your Drawing
We read and edit digital drawings in-house and machine each shank to the dimensions your feeder actually runs.
Seats and Clamp Faces
Blade seats and clamp faces are machined so blades pull down evenly and hold alignment through hard reversal.
Matched Across Gob Layouts
Shanks for SG, DG, TG and QG mechanisms are machined as matched sets, so every blade pair closes on the same setting.
Interchangeable Fit
Built to interchange with the shear mechanism already on your feeder, so fitting a replacement does not turn into a rework job.
Gallery
Shear Shanks for IS-Machine Feeders in Detail
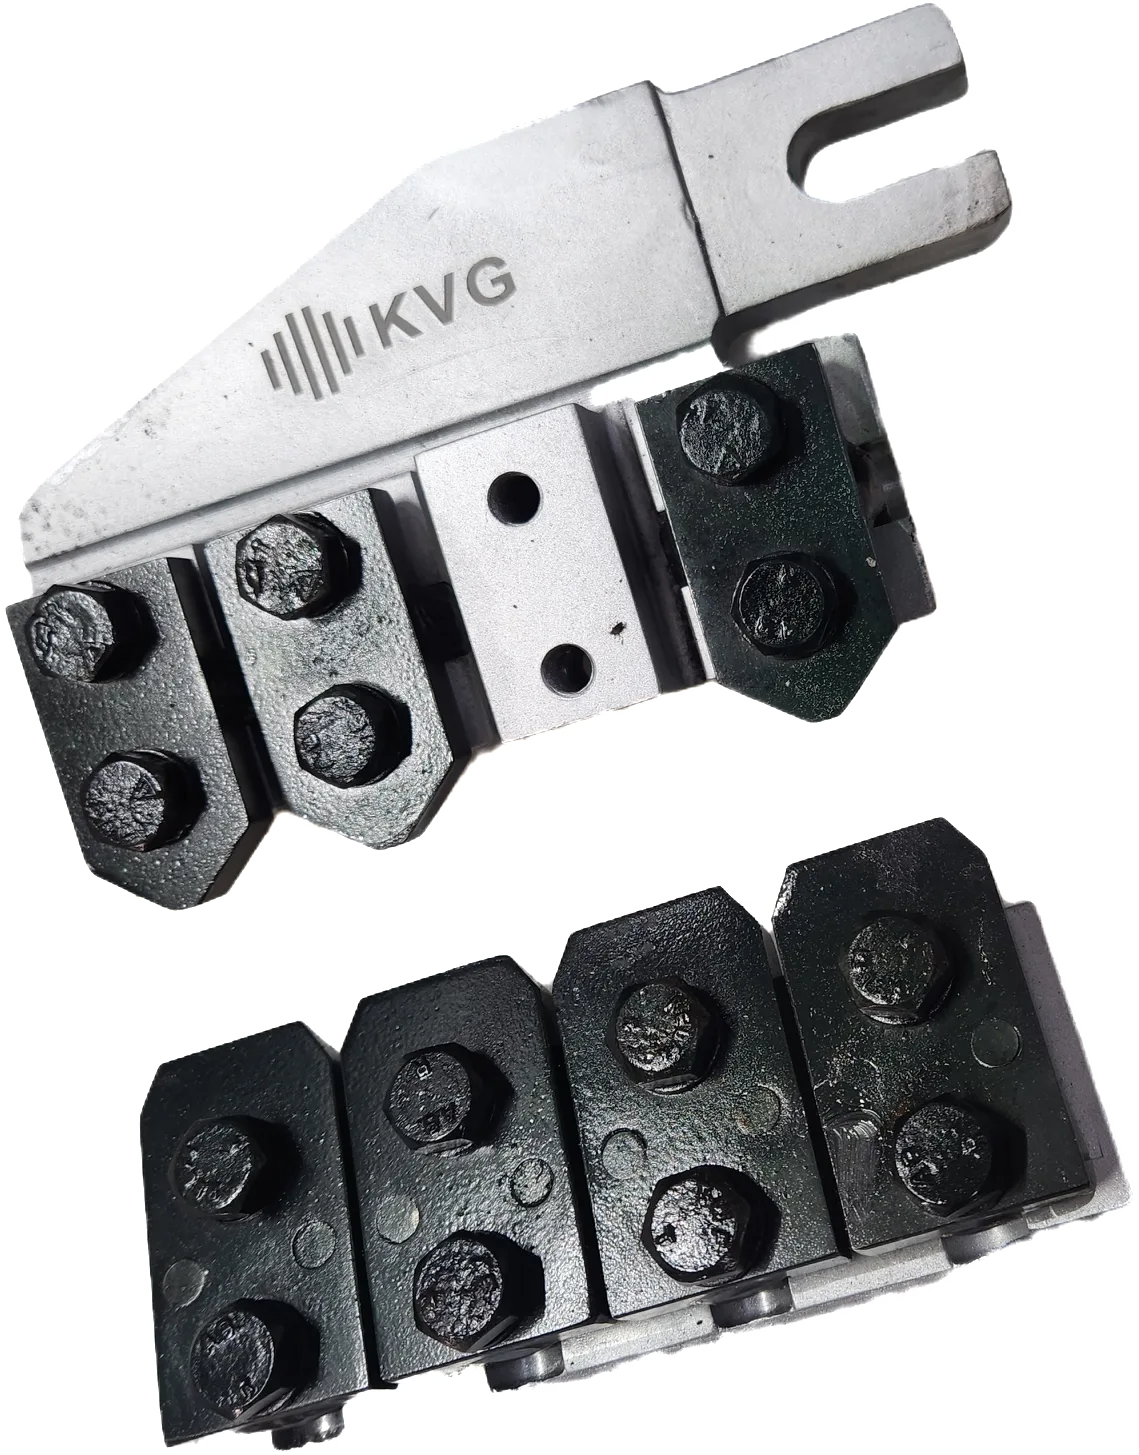
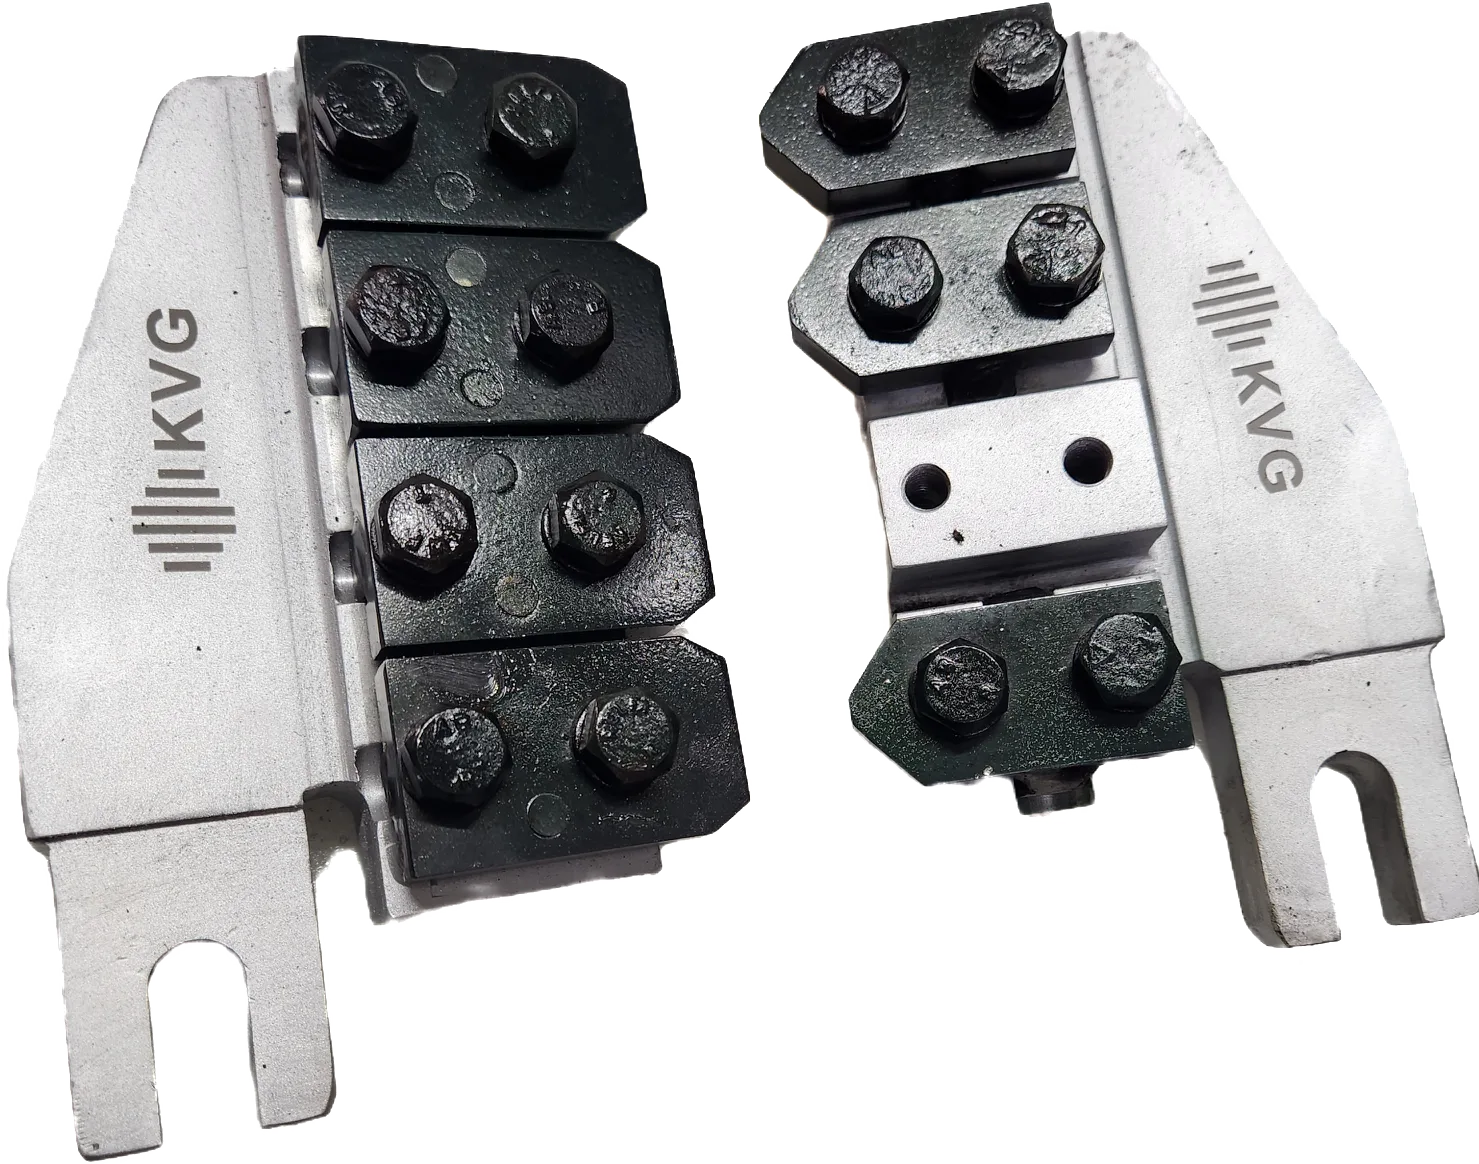
Photographs show KVG-manufactured parts. Configurations are made to your drawing — send us your part reference for an exact quote.